Family Owned & Operated Since 1980
Clear Water Filtration delivers specialized water treatment solutions for manufacturing and industrial facilities throughout Vermont. Since 1980, our family-owned company has partnered with some of the state's most respected manufacturers and industrial operations to solve complex water quality challenges that directly impact production quality, equipment longevity, and operational efficiency.
Schedule a Facility Assessment Request ServiceIndustrial Water Treatment Expertise
Manufacturing operations depend on water—for cooling, processing, cleaning, and countless other applications. At Clear Water Filtration, we've spent more than four decades perfecting water treatment solutions for industrial facilities that demand precision, consistency, and reliability.
Our work with Vermont's leading manufacturers has taught us that industrial water treatment isn't one-size-fits-all. A precision plastics facility has different needs than a brewing operation, and a pharmaceutical manufacturer requires different water specifications than a machining shop. We approach every industrial project with this understanding, designing custom solutions that address your specific process requirements.
Vermont's manufacturing sector faces unique water quality challenges. From semiconductor facilities requiring ultrapure process water to food processing plants demanding consistent water chemistry, the stakes are high. Poor water quality can halt production lines, damage expensive equipment, and compromise product quality. Our team brings over four decades of experience solving these exact problems for industrial operations across the Green Mountain State.
We understand that every hour of downtime costs money. That's why we've built our commercial water treatment services around rapid response, reliable systems, and redundant designs that keep your operations running. When Burlington, Montpelier, Rutland, and Essex manufacturers need water treatment expertise they can count on, they turn to Clear Water Filtration.
What Sets Us Apart
Our manufacturing water treatment capabilities are built on decades of experience serving Vermont's industrial community. As an Authorized, Independent Kinetico Dealer for over 30 years, we bring proven commercial-grade equipment backed by industry-leading warranties to every industrial installation.
Process Water Engineering
Different manufacturing processes demand different water quality specifications. Our engineering team works closely with your operations staff to understand exact requirements and design systems that consistently deliver water meeting or exceeding your specifications.
Before designing any industrial water treatment system, we conduct thorough assessments including:
Our comprehensive water testing evaluates your source water for hardness, pH, total dissolved solids, iron, manganese, turbidity, and any contaminants specific to your process concerns. This baseline understanding drives system design.
We document the water quality specifications for each process in your facility—from boiler feed water requirements to rinse water standards to product ingredient specifications. This mapping ensures every application receives appropriately treated water.
Understanding peak demand, average usage, and surge requirements helps us size equipment properly and design systems that won't become bottlenecks in your operation.
For manufacturers with strict quality management systems, we design solutions that integrate with your monitoring and documentation requirements.
Our industrial water treatment solutions serve diverse manufacturing sectors across the Green Mountain State:
Every manufacturing facility presents unique water treatment challenges. Our approach combines decades of field experience with current technology to deliver solutions that work.
Our Process
When you partner with Clear Water Filtration for manufacturing water treatment, here's what to expect:
Our technical team visits your facility to understand your operation, evaluate existing water infrastructure, and document specific challenges. We review process specifications, quality requirements, and operational constraints.
Comprehensive laboratory analysis of your source water establishes baseline conditions and identifies treatment requirements. For facilities with multiple water sources, we test each supply.
Based on assessment findings, we engineer a treatment solution addressing your specific needs. Designs incorporate appropriate redundancy, monitoring capabilities, and capacity for future growth.
We specify commercial-grade equipment from trusted manufacturers including Kinetico, Hallett, Viqua, and Stenner. Equipment selections balance performance requirements, operational costs, and maintenance accessibility.
Our licensed plumbers and water treatment technicians handle professional installation, startup, and commissioning. We verify system performance against specifications before handoff.
Your operations team receives thorough training on system operation, routine maintenance, and troubleshooting. We provide complete documentation for your quality systems.
Treatment Technologies
Meeting stringent manufacturing water specifications requires appropriate treatment technologies properly applied. Here's an overview of solutions we commonly deploy for industrial facilities in Vermont.
Hard water containing elevated calcium and magnesium causes scale buildup in boilers, heat exchangers, cooling towers, and process equipment. Scale reduces efficiency, increases energy costs, and eventually damages equipment requiring expensive repairs or replacement.
Industrial Water Softening
Commercial-grade Kinetico softening systems remove hardness minerals through ion exchange. Our industrial softeners feature:
Scale Inhibition Systems
Where complete softening isn't practical, scale inhibition technologies can protect equipment without removing minerals from water.
Particulate matter, sediment, and suspended solids must be removed for many manufacturing processes. Our filtration solutions include:
Multimedia Filtration
Multi-layer filter beds remove particles down to 10-15 microns, protecting downstream treatment equipment and improving process water quality.
Cartridge & Bag Filtration
For finer filtration requirements, cartridge and bag filter housings provide particle removal down to sub-micron levels. We design these systems for easy maintenance access and low operating costs.
Automatic Backwash Systems
Self-cleaning filter systems reduce maintenance requirements for high-flow applications, automatically removing accumulated solids without operator intervention.
Many industrial processes require precisely controlled chemical addition. Stenner chemical feed systems provide accurate, reliable dosing for:
Our technicians install, calibrate, and maintain chemical feed systems for consistent, accurate operation.
When your process demands high-purity water with minimal dissolved solids, reverse osmosis treatment provides exceptional water quality. Our commercial RO systems deliver:
Viqua ultraviolet disinfection systems eliminate bacteria, viruses, and other microorganisms without chemical addition. For food processing, beverage production, and pharmaceutical manufacturing, UV provides chemical-free disinfection meeting regulatory requirements.
Applications requiring ultrapure water—laboratory use, electronics manufacturing, pharmaceutical production—benefit from deionization systems removing virtually all dissolved minerals. We design DI systems as standalone units or polishing treatment following reverse osmosis.
System Reliability
Manufacturing operations can't afford water treatment system failures during production. Our system designs prioritize reliability through redundancy, quality components, and accessible maintenance.
Commercial Equipment Partners
Industrial water treatment demands commercial-grade equipment built for continuous operation in demanding environments. We specify and install equipment from manufacturers with proven track records in industrial applications.
Proven Track Record
Since 1980, Clear Water Filtration has built relationships with Vermont manufacturers who depend on us for critical water treatment services. Our family-owned company takes pride in supporting the state's manufacturing economy with reliable, expert service.
Our commercial client roster includes some of Vermont's most respected names across diverse industries:
These relationships span years—in many cases, decades. When Vermont manufacturers need water treatment expertise, they call Clear Water Filtration because we've earned their trust through consistent, reliable service.
Since 1980, we've solved water treatment challenges for manufacturing facilities across Vermont. Our technicians understand industrial applications and the critical importance of reliable water quality.
Our team includes licensed plumbers qualified to work on industrial water systems. We handle installations properly, meeting all applicable codes and standards.
Manufacturing doesn't stop for business hours. Our emergency service runs seven days a week, 7am to 9pm, because we understand production schedules don't always align with standard service windows.
We manufacture many components and custom assemblies in-house at our Waitsfield facility. This capability means faster response times and better solutions for unique industrial requirements.
As members of the Vermont business community—including the Mad River Chamber of Commerce—we understand local conditions, regulations, and resources. We maintain relationships with engineers, contractors, and state regulators that benefit our commercial clients.
Emerging Contaminants
Emerging contaminants including PFAS and PFOA compounds present growing concerns for Vermont manufacturers. These persistent chemicals, found in some industrial water supplies, may impact product quality, regulatory compliance, and environmental responsibilities.
Clear Water Filtration holds multiple government contracts for PFAS/PFO Treatment, bringing proven expertise to industrial facilities facing these challenges. Our treatment solutions effectively remove PFAS compounds from process water through specialized filtration and treatment technologies.
Manufacturing facilities may encounter PFAS in:
Our engineers evaluate PFAS concerns within your overall water treatment strategy, recommending appropriate testing, treatment, and monitoring.
Learn MoreOur founder, Jen Fleckenstein, serves on the Technical Advisory Committee to the Governor of Vermont, advising on water quality concerns and issues affecting the state. This involvement keeps us at the forefront of water quality science, regulations, and best practices—expertise we bring to every commercial project.
Service & Maintenance
Water treatment systems require ongoing maintenance to deliver consistent performance. Our commercial service programs provide the regular attention your systems need while minimizing demands on your operations staff.
For critical systems requiring frequent attention, monthly service visits include filter changes, chemical replenishment, calibration verification, and performance testing.
Standard commercial service programs include quarterly visits for routine maintenance, inspection, and performance verification.
Systems with lower maintenance requirements benefit from comprehensive annual service visits combining routine maintenance with detailed inspection and testing.
Semi-annual service programs balance maintenance needs with operational efficiency for many industrial applications.
Our service technicians are trained specifically for industrial applications. Service visits typically include:
When equipment problems threaten production, our emergency service provides rapid response. Available seven days a week from 7am to 9pm, our technicians carry parts inventory and tools to resolve most issues on the first visit.
Manufacturing emergencies don't wait for business hours. Call us immediately when water treatment issues threaten your production.
802-496-5544
Where We Serve
From our home base in Waitsfield, VT, we provide water treatment services throughout the Green Mountain State. Each community has its own water quality characteristics based on local geology and water sources - and after 45 years, we've tested thousands of wells across Vermont and understand the regional variations that affect which treatment approaches work best.
Hear From Your Neighbors

Bill Cherry
Switchback Brewing

Lindsay Kurrle
Community Relations Coordinator

Win Smith
President
Ken Bisceglio
Regional Manager
We're Here to Help
Let's Get Started
Your manufacturing operation deserves water treatment partners who understand industrial requirements, respond when you need them, and deliver reliable results. Clear Water Filtration has served Vermont manufacturers since 1980, building relationships through consistent performance and genuine expertise.
We're not just another vendor—we're neighbors who've been part of the Vermont business community for over four decades. When Jen advises the Governor of Vermont on water quality issues, when we sponsor local schools and contribute to the Vermont Foodbank, when we show up for emergency service calls at 8pm on a Saturday—that's who we are.
Our manufacturing water treatment services combine this local commitment with technical capabilities matching any water treatment company in the region. From process water engineering to emergency repairs, from new facility design to ongoing maintenance, we deliver what your operation needs.
After over 40 years serving Vermont manufacturers, we've learned that every facility is unique. Let us learn about yours and show you what properly engineered water treatment can do for your operation.
802-496-5544 Get Started Today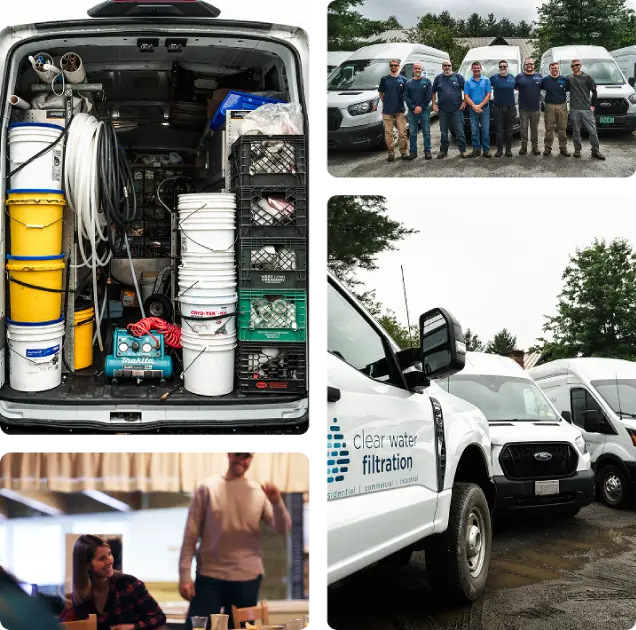
Explore More
Commercial water treatment engineered for Vermont businesses, plus the five industries we cover in detail. See everything on the commercial water treatment hub.
Agriculture Food & Beverage Healthcare & Labs Resorts & Hospitality Commercial Water Treatment Commercial PFAS Treatment
© Red Barn Media Group 2026